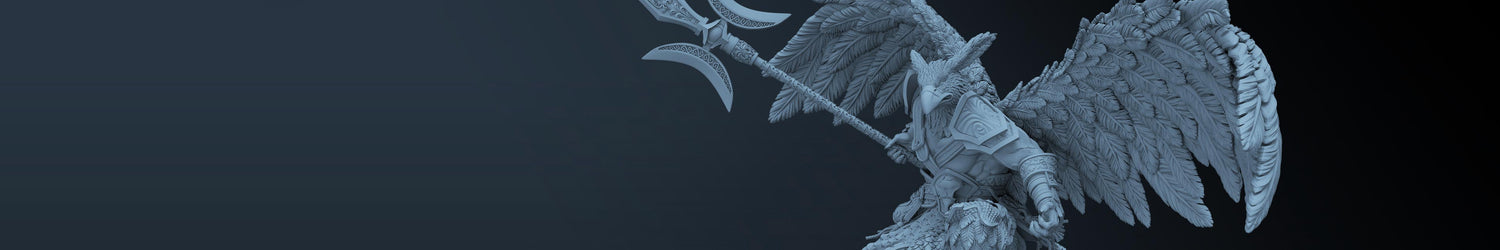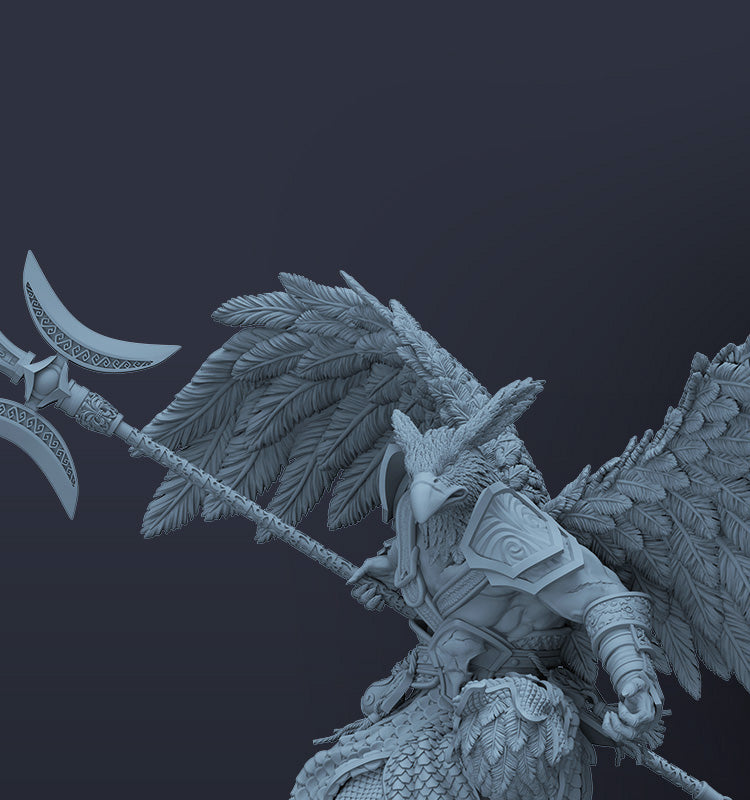


I had to increase the exposure and light off time vs. Instructions using my M7 Max, but the results are very impressive!

Couldn't load pickup availability




Supports detach effortlessly with minimal post-processing, while maintaining structural integrity even in micro-scale parts and thin-walled structures.


Anycubic Tough Resin 2.0 delivers comprehensive upgrades in tensile strength and flexibility, achieving the optimal balance of high strength and exceptional toughness. Ideal for diverse professional applications, including structural components, industrial prototypes, jigs, and fixtures.


Clear texture details. Smooth and fine texture. High degree of overall fidelity

Anycubic resin features a specially engineered low-odor formulation, delivering zero irritation for a pleasant, comfortable printing experience.

It is compatible with all LCD/DLP printers that use 405nm UV light curing technology and works best with Anycubic LCD printers.


| Printer Model | Layer Thickness | Exposure Time | Light-Off Time | Bottom Exposure Time | Bottom Layers | Anti-Aliasing Level | Z Lift Distance | Z Lift Speed | Z Retract Speed |
| Photon P1 | 0.05 mm | 2.1 s | 2 s | 15 s | 1 | 4 | 5 mm | 3 mm/s | 3 mm/s |
| Photon Mono M7 | 0.05 mm | 2.2 s | 0.5 s | 25 s | 4 | 1 | 8 mm | 6 mm/s | 6 mm/s |
| Photon Mono M7 Pro | 0.05 mm | 1.8 s | 0.5 s | 25 s | 3 | 1 | 8 mm | 6 mm/s | 6 mm/s |
| Photon Mono M7 Max | 0.05 mm | 2 s | 0.5 s | 30 s | 5 | 1 | 8 mm | 6 mm/s | 6 mm/s |
| Photon Mono M5 | 0.05 mm | 2.8 s | 0.5 s | 25 s | 5 | 1 | 8 mm | 5 mm/s | 6 mm/s |
| Photon Mono M5s | 0.05 mm | 2.8 s | 0.5 s | 25 s | 5 | 1 | 8 mm | 5 mm/s | 6 mm/s |
| Photon Mono M5s Pro | 0.05 mm | 3.6 s | 0.5 s | 30 s | 5 | 1 | 8 mm | 6 mm/s | 6 mm/s |
| Photon Mono 4 | 0.05 mm | 2.8 s | 1 s | 30 s | 5 | 1 | 6 mm | 4 mm/s | 6 mm/s |
| Photon Mono 4K | 0.05 mm | 2 s | 0.5 s | 40 s | 6 | 1 | 6 mm | 4 mm/s | 6 mm/s |
| Photon Mono 4 Ultra | 0.05 mm | 2.6 s | 1 s | 30 s | 5 | 1 | 5 mm | 8 mm/s | 8 mm/s |
| Photon Mono 2 | 0.05 mm | 2.5 s | 1 s | 25 s | 5 | 1 | 6 mm | 4 mm/s | 6 mm/s |
| Photon Mono X2 | 0.05 mm | 2.5 s | 0.5 s | 20 s | 5 | 1 | 8 mm | 2 mm/s | 3 mm/s |
| Photon Mono X 6K | 0.05 mm | 2 s | 0.5 s | 25 s | 6 | 1 | 8 mm | 2 mm/s | 3 mm/s |
| Photon Mono X6Ks | 0.05 mm | 2.5 s | 0.5 s | 20 s | 5 | 1 | 8 mm | 3 mm/s | 4 mm/s |
| ANYCUBIC Photon M3 Max | 0.05 mm | 3 s | 2.5 s | 35 s | 6 | 1 | 10 mm | 2 mm/s | 3 mm/s |
| ANYCUBIC Photon M3 Premium | 0.05 mm | 2.5 s | 0.5 s | 25 s | 2 | 1 | 8 mm | 6 mm/s | 6 mm/s |
1. Before Use
Shake liquid resin well
Clean resin tank and build plate
Ensure tank bottom remains highly transparent
Confirm release film is undamaged
Verify correct print parameter settings
Recommended printing environment: 20-35°C (to prevent temperature-related failures)
2. During Use
Unscrew bottle cap and remove sealing film
Pour resin into tank without exceeding max fill line
3. After Printing
Use included tools for post-processing:
Scraper / Flush cutters / Tweezers / Gloves / ≥95% IPA cleaning solution
4. Post-Processing
A. Remove models from build plate using scraper; remove supports
B. Clean models in Anycubic Wash & Cure machine for ~10 minutes (use ≥95% alcohol or cleaner)
C. Dry models: Air-dry, blow-dry, or use drying chamber (prevents water absorption/cracking)
D. Secondary curing: Cure models for 3-5 minutes
E. Resin recycling: Filter through 100-mesh sieve
Notes
Material properties may vary based on:
Printing equipment
Post-curing methods
Testing instruments
For safety data/certifications (MSDS, REACH, RoHS, EAN, TDS): Refer to product documentation
Contact us with any issues
Overall rating: 4.6 / 5 from 5 reviews.
I had to increase the exposure and light off time vs. Instructions using my M7 Max, but the results are very impressive!
great resin and delivery
Good resin, but still warps marginally
Familiar with this product and can report that it is excellent. Ordering and delivery were easy and reliable, this is the best location for AnyCubic products in the UK.

Finally found the resin I need. Strong and suitable for moving parts but with no real loss of detail :)